AI-Based PPE Monitoring System
A large industrial manufacturing facility faced challenges in ensuring consistent Personal Protective Equipment (PPE) compliance across its workforce. Manual supervision was ineffective, leading to safety risks, compliance issues, and potential regulatory penalties.
Problem Statement
The client struggled with
 Inconsistent PPE compliance across departments. Dependence on manual monitoring and safety officers. Lack of real-time alerts for violations. Difficulty in maintaining audit-ready compliance records. Increased risk of workplace accidents and downtime.
Traditional safety monitoring methods were reactive, error-prone, and resource-intensive.
Solution Implemented
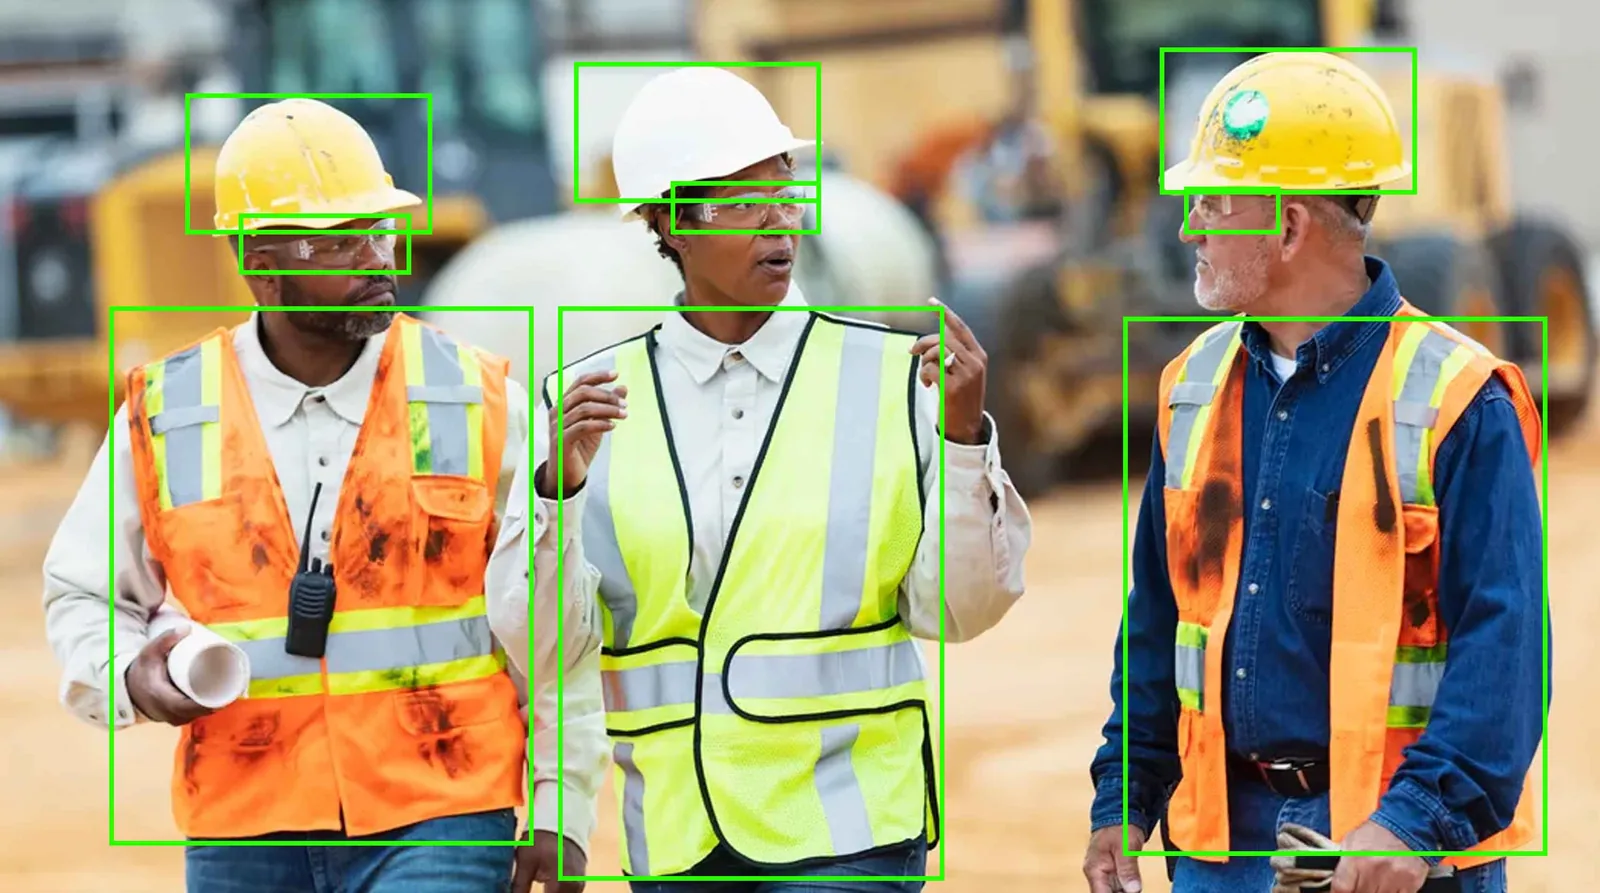
RDL Technologies deployed an AI-Based PPE Monitoring System, an intelligent solution leveraging computer vision and machine learning to automate safety compliance. The system uses existing CCTV infrastructure to monitor workers in real time and detect whether required PPE is being worn.
How the System Works
 Live Video Input
CCTV/IP cameras capture real-time footage across facility zones.
 AI-Based Detection
AI models analyze video streams to identify workers and PPE usage.
 Compliance Verification
The system checks for required safety gear such as helmets, gloves, vests, and masks.
 Instant Alerts
Violations trigger audio/visual alerts and notifications to supervisors.
 Data Logging & Reporting
All incidents are recorded with timestamps and visual evidence for audits.
Key Features
Real-Time PPE DetectionWorker Identification (RFID / Face Recognition)Zone-Based Safety RulesEdge & Cloud AI DeploymentAutomated Alerts (Mobile & Dashboard)Compliance Dashboard with AnalyticsERP/MES IntegrationThe system also provides dashboards showing compliance trends, violation logs, and predictive safety insights.
Technology Stack
AI Models YOLOv8, SSD, TensorFlow.
 Hardware
NVIDIA Jetson, Intel NUC, IP Cameras
 Platform
Web Dashboard + Mobile App
 Integration
REST APIs, MQTT, ERP & MES systems
Results & Impact
 Improved Safety Compliance
● Continuous monitoring ensures workers follow PPE protocols at all times.
● Eliminates reliance on manual supervision
 Reduction in Workplace Accidents
● Early detection of violations prevents potential hazards.
● Enhances overall workplace safety.
 Real-Time Decision Making
● Instant alerts enable quick corrective action
 Audit-Ready Documentation
● Automated logs simplify compliance with OSHA, ISO 45001, and factory regulations.
 Operational Efficiency
● Reduces manual inspection efforts.
● Optimizes safety team productivity.
Business Benefits
 Lower accident-related costs and downtime. Increased workforce accountability. Better compliance with regulatory standards. Data-driven safety improvements. Scalable across multiple plants and locations.
Use Cases / Industries
Construction Sites. Manufacturing Plants. Mining Operations. Chemical & Pharma Industries. Warehousing & Logistics. Conclusion
The AI-Based PPE Monitoring System transforms traditional safety practices into a proactive, automated, and data-driven approach. By leveraging AI and IoT, organizations can ensure 100% visibility, improved compliance, and a safer work environment, while significantly reducing operational risks.