The Challenge
- Human error, Not 100% Accurate readings noted and Only Specific Parameters are Captured.
- Limited visualization only provided localized view of the system.
- Invisibility of wastage, and any breakdown will lead long time to analyze.
- Predicting the root cause and anomaly is not possible.
- There are no proactive failure and disturbance alarms.
- Meter data used only for billing, cannot help in analysis like demand analysis, energy audit, pinpointing losses, etc.
Benefits
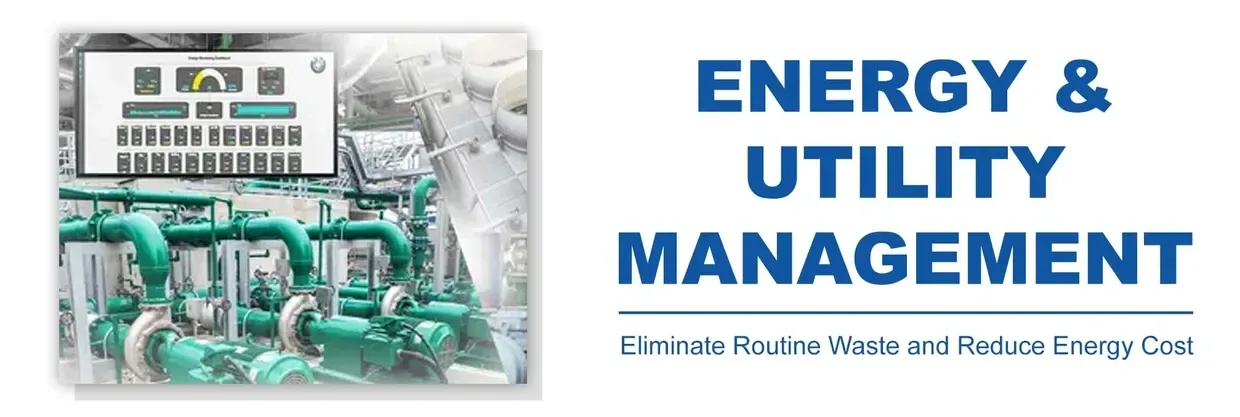
- Centralized monitoring with automatic pre-warning alarm.
- Real-time End to end traceability of consumption.
- Visibility of utilization of utilities and track them to set baseline values saving from penalties.
- Improve stand-by operation & energy cost per unit.
- Eliminate routine waste & reduce energy cost.
- Proactive alerts of failure and disturbances.
- Enable management with KPI views to set Utility Goals.
- Reduction of production costs and Optimize Energy Efficiency by 8 - 10%.
- Early detection of potential problems leads to increased uptime Maintenance activities, improved Safety & longer machine lifespan.
- Minimize Unplanned Downtime and reduce the maintenance costs & time.
- Remote & real-time monitoring system helps in achieving high operation efficiency.
Asset Covered
- CNC Machines
- Welding machines
- Compressor
- Oven.
- Chillers
- ETP Plant Pump
- Dryers
- Pretreatment Boilers Unit
- Cooling tower
- AHU’s
- DG Sets
- Paint Booth
- Incomer
- Distributor
Machine Data
- Voltage
- Current
- Power Factor
- Power
- Energy
- Harmonics
- Temperature
- Air quality parameters
- Humidity
- Pressure
- GAS Consumption
- VFD Frequency
- Valve position
- Water flow